
























Article Contents:
- Cenote HL-029 inset wooden handle: what exactly the buyer receives
- Why 80×20×66×11 mm cannot be automatically sent to the milling specialist
- What size to provide to the cabinetmaker before milling begins
- 16 mm facade and 11.5 mm recess: what the remaining 4.5 mm means
- Why it is better to choose Cenote before the final painting of facades
- Buy handles in advance or after manufacturing the facades
- The visible part of Cenote protrudes by 9 mm: inset does not mean fully flush
- Cenote handle for a cabinet: when 9 mm matters more than the front 80 mm
- Beech or oak: the material is chosen before the handles are sent to the common finishing cycle
- Unpainted HL-029 or finished Cenote HL-029M
- Twenty Cenote: why one control fitting is needed first
- What to record in the map of one test fitting
- The coordinates of the handle on the facade are a separate task from the diameter of the recess
- What to check on the back side of the facade before making the Ø67 recess
- Glue and fitting: why the installation description does not become a universal technology
- What to write in the specification for Cenote HL-029
- When not to order Cenote HL-029 yet
- Where to buy Cenote HL-029 and other wooden furniture handles
- Questions before ordering Cenote HL-029
- Why does the product card show 66×11 and at the same time Ø67×11.5 mm?
- D=66 — is this the cutter diameter?
- E=11 — is this the routing depth?
- What size should be provided to the CNC machine?
- Can Cenote be installed on a 16 mm cabinet front?
- What does the calculation 16 − 11.5 = 4.5 mm mean?
- Does the handle fully recess into the cabinet front?
- Do I need to buy the handles before painting?
- Can I paint the fronts first and then do the routing?
- Is one test fitting enough for twenty facades?
- Is the glue included with the handle itself?
- What is the difference between HL-029 and HL-029M?
- How to choose between beech and oak?
- Will Cenote fit a cabinet in a narrow niche?
- What should be checked on the day of CNC startup?

The facades are already in production. Before priming and enameling, the cabinetmaker asks for one number: what diameter and what depth to program into the CNC for Cenote HL-029. In the handle's card, the product line 80 × 20 × 66 × 11 mm is visible, so it seems natural to send to the workshop: "mill Ø66 to a depth of 11 mm."
But the mounting description of the same Cenote HL-029 specifies a different pair: a recess of Ø67 mm with a depth of 11.5 mm. This is not a reason to declare D=66 and E=11 as erroneous. This is a reason to stop interpreting the product's letter dimensions as a mounting cutout without a drawing.
For furniture production, the working sequence should be as follows: select a specific Cenote HL-029 → obtain the current drawing → compare the product line with the mounting description → perform one control fitting → only then start the series of facades and final finishing. An error on one test sample is local. An error in twenty painted facades is already a rework of the furniture.

Inset wooden handle Cenote HL-029: what exactly the buyer receives
Cenote HL-029 — flush-mounted wooden furniture handle. The current product card specifies beech and oak, 'Prestige' sanding quality, unfinished supply, and the option to choose the quality of edge gluing for future finishing.
| Parameter | Cenote HL-029 |
|---|---|
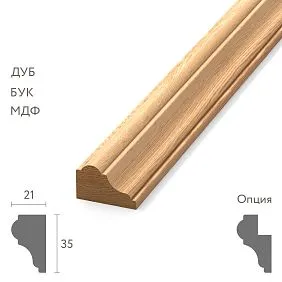
| Product dimensions A × C × D × E | 80 × 20 × 66 × 11 mm |
| Type | flush-mounted wooden furniture handle |
| Material | Beech / Oak |
| Sanding | «Prestige» |
| Supply | Unpainted |
| Minimum front panel thickness | From 16 mm |
| Mounting recess as described | Ø67 × 11.5 mm |
| Visible protrusion after installation | 9 мм |
| Average production time for made-to-order items | 5–10 days |
The product card separately explains the installation: the handle is glued into a prepared mounting recess. Therefore, for a cabinetmaker, not only the visible 80 mm and appearance are crucial, but also the actual geometry of the recess.
If the model is already approved by the project, Buy Cenote HL-029 recessed wooden handle it is better to do so before final processing of the entire batch of facades, so that the workshop can check the physical part and the current drawing.
Why 80×20×66×11 mm cannot be automatically sent to the milling operator
The string A × C × D × E = 80 × 20 × 66 × 11 mm describes the product in the manufacturer's notation. It does not give the right to say on its own:
D=66, so the hole should be Ø66;
E=11, so the recess depth should be 11 mm.
The Cenote mounting description separately specifies Ø67 mm and 11.5 mm. Therefore, we have two sets of parameters with different purposes.
The most dangerous mistake is not the difference of one millimeter in diameter and half a millimeter in depth by itself. What is dangerous is that the furniture maker starts processing a batch without understanding what geometry each number describes.
For production, it is useful to clearly separate the concepts in the specification:
| What | Value |
|---|---|
| Product dimension string | 80 × 20 × 66 × 11 mm |
| Mounting recess per card description | Ø67 × 11.5 mm |
| Final size for CNC | per current drawing and test fit |
Thus, the operator has no temptation to take D and E as a ready-made technological map.
Our factory also produces:




What size to provide to the furniture maker before milling begins
There is no need to choose between 66×11 and 67×11.5 "by common sense." A short technical verification cycle is required.
First, open the current card for the specific article HL-029, not a similar handle. Then take the product drawing. On it, you need to find exactly the mounting dimensions: the diameter of the seating area, depth, position of the front part, and geometry of the rear part.
After that, three things are checked:
- the product's dimensional table;
- the textual mounting description;
- the dimensional notations on the drawing.
If the drawing confirms Ø67 × 11.5 mm, this exact mounting size is transferred to the technological map. If the drawing contains other current information, production must not choose a version independently — confirmation from the manufacturer is required before the batch is launched.
The correct notation for the furniture maker is not "Cenote 66×11," but:
Cenote HL-029. Product size 80×20×66×11 mm. The mounting recess must be made only according to the current installation drawing; the card text indicates Ø67×11.5 mm. Before the series — a control fit.
Such a line cannot be accidentally read as permission to program Ø66.
Get Consultation
Facade 16 mm and recess 11.5 mm: what the remaining 4.5 mm means
The card allows installing Cenote on furniture facades with a thickness of 16 mm or more. If you take the minimum 16 mm and the mounting depth of 11.5 mm from the description, the arithmetic gives:
16 − 11.5 = 4.5 mm.
These 4.5 mm are the nominal geometric thickness remainder. This is not an independently calculated load-bearing capacity and not a guarantee of facade strength.
Why can't you go beyond simple arithmetic? The facade may be made of solid wood, MDF, or another structure; the actual thickness may differ from the nominal one; there may be milling, a frame, a hinge recess, a technological groove, or another element on the reverse side. Machine tolerances and the actual processing depth matter.
Therefore, in the technical card, next to "facade ≥16 mm," there should be a line:
check the actual thickness and the absence of conflicting processing in the Ø67 area.
If a 16 mm facade already has deep processing on the reverse side, the figure of 4.5 mm does not automatically allow combining two recesses.
Why Cenote is better to choose before final painting of facades
An inset handle requires noticeable processing of the front part of the furniture. Doing such an operation after the final enamel can only be a deliberate technological process, not because the handle was chosen at the last moment.
Before finishing, it is easier to perform a test cut, check the position, remove technological traces, and integrate further preparation into the overall facade cycle. If an error is found on a raw workpiece, its consequences are usually more localized than on a fully painted door.
For Cenote, the sequence is especially important:
handle model → drawing → coordinates on the facade → test cut → check with the physical handle → serial processing → surface preparation → finish → final installation.
This is not an instruction on milling modes. Speed, tool, allowances, and coating processing remain the task of furniture production. What matters to the buyer is different: do not change the handle model after the geometry has already been incorporated into the facades.
If the project is still comparing options, buy inset wooden handles it is better from a professional selection before launching the furniture batch.
Buy handles in advance or after manufacturing the facades
For surface-mounted hardware, the choice can sometimes be postponed to a later stage. For Cenote, the risk is higher: the recess is part of the facade itself.
A physical handle before the series gives the cabinetmaker several checks at once. It can be applied to a test sample, the actual fit can be assessed, the visible protrusion can be checked, and it can be ensured that the grip is comfortable at the chosen height and that adjacent elements do not conflict.
This is especially important when many identical doors and drawers are produced. One incorrectly interpreted parameter is copied by the machine without error—but that is exactly why the mistake becomes serial.
A rational approach for a furniture workshop: buy one or several Cenote before starting CNC, approve the technical card, and order the main quantity after confirming the result or in one batch if the project's logistics require it.
The visible part of Cenote protrudes by 9 mm: recessed does not mean "completely flush"
Cenote is recessed into the facade, but the card directly states that its visible part rises above the surface by approximately 9 mm.
This figure answers a different question than the recess depth. The 11.5 mm refers to the mounting recess, while the 9 mm refers to the visible part after installation.
Checking the 9 mm is useful in places where the facade works near an obstacle:
- near a wall or side panel;
- on adjacent doors;
- on drawers with a small gap between fronts;
- next to a decorative molding;
- in a narrow passage;
- near a pull-out internal system.
To check, it is enough to make a side template or attach a real handle to a test facade. Do not assume that the word "recessed" automatically means zero protrusion.
Cenote handle for a cabinet: when 9 mm matters more than the frontal 80 mm
On a regular hinged cabinet, the buyer first notices the round shape and the overall size of 80 mm. But in a narrow niche or near a side wall, the 9-millimeter protrusion can become critical.
Suppose the door opens toward a wall and the distance to it is small. The frontal width of 80 mm by itself does not describe the conflict: the handle is located on the plane of the door. And the 9 mm protrusion shows how much the hardware extends from this plane into the room.
The same applies to two adjacent facades that pass close to each other when opening. You need to check the trajectory, not just look at the frontal sketch.
A request for "wooden cabinet handles" may lead to Cenote as an option, but the model cannot be automatically recommended for sliding doors or any narrow system. For such furniture, first check the structural gaps and trajectories.
Beech or oak: the material is chosen before handles are sent to the common finishing cycle
HL-029 is supplied unfinished and is available in beech and oak. For furniture where handles need to be painted to match the facades or have their own project finish, this is convenient: the finish can be coordinated together with the facade sample.
But the material should be fixed before ordering the series. If some handles are beech and others are oak, the same coating color does not make the blanks absolutely identical in structure and preparation.
For the production sheet, a line is sufficient:
Cenote HL-029 / beech or oak / Prestige / selected splicing quality / quantity.
If a custom color is needed, the logical commercial path is buy unpainted wooden handles and include them in the project's finishing technology.
Unfinished HL-029 or finished Cenote HL-029M
Cenote has a separate version HL-029M with factory coating. It retains the same dimensional format of 80 × 20 × 66 × 11 mm, but is sold as a ready-painted handle. For HL-029M, ready-made coating options are used; in current STAVROS materials, white, brown, transparent, and black finishes are shown.
The fork is simple:
need a custom project color or a unified finish together with the furniture → HL-029;
a ready-made factory coating is suitable → check HL-029M.
However, switching to HL-029M does not cancel the installation check. Before milling, you still need to use the current drawing of the exact model that will actually be installed.
If the ready color suits the project, you can look at the ready-made wooden handle Cenote HL-029M as an alternative to the unpainted version.
Twenty Cenote: why one control fit is needed first
Suppose a cabinetmaker makes 12 doors and 8 drawers. A total of 20 handles are needed.
The most expensive mistake is not buying twenty handles. The most expensive mistake is machining twenty fronts to a size that no one has checked on a physical part.
The control scheme should be as follows:
1 Cenote → 1 test blank → fit check → program fixation → processing 20 facades.
On the sample, they check not only that the handle fits. You need to make sure it sits at the intended depth without skew, the visible part is in the correct position, the glue has a working contact area, and there is no dangerous conflict on the back side of the facade.
If the facades are of different types — for example, some doors are 18 mm, some drawers are 20 mm — one test piece is sufficient only when the geometry of the installation area is truly identical. Otherwise, control samples are made for each distinct structural type.
The CNC machine repeats the program very precisely. That is why checking the program before the series is more important than the processing speed of the batch itself.
What to record in the card for one test fit
For the control sample to make sense, the result must be written down, not left at the level of "the master said it's fine."
The card records:
| Field | What to record |
|---|---|
| Handle model | Cenote HL-029 |
| Actual facade | material and thickness |
| Product size | 80 × 20 × 66 × 11 mm |
| Mounting selection | According to the approved drawing |
| Card text | Ø67 × 11.5 mm |
| Cutter / program | Internal shop code |
| Position by X/Y | by facade map |
| Placement result | accept / adjust |
| Visible protrusion | check on physical part |
| Approval date | ___ |
If the program changes after testing, the CNC file version must also change. Otherwise, production can easily revert to the old version when rerunning.
For a series of several kitchens or cabinets, such a map becomes a reference that can be used when reordering HL-029.
The handle coordinates on the facade are a separate task from the diameter of the recess.
Even a perfect Ø67 won't save the facade if the handle is placed at the wrong height or too close to the edge.
The position of Cenote is set on the facade drawing with separate coordinates. The facade frame, panel, internal milling, hinges, and other decor must be considered. On multiple doors, handles should form a consistent rhythm.
Do not choose a coordinate based on the principle of "center of the circle offset 50 mm from the edge" if such a dimension is not in the project. Each piece of furniture has its own geometry.
For drawers, it is useful to check the grip on a real cabinet: the same graphic coordinate may be inconvenient on low and high fronts. This is already an ergonomic issue that is solved with a mockup, not a handle characteristic.
What to check on the back side of the facade before milling Ø67
On the front side, Cenote occupies a compact circular area. But milling to a depth of 11.5 mm works within the facade thickness, so before starting the CNC, you need to check what is at the same coordinate on the back.
For a hinged door, this could be a hinge cup, its mounting plate, or frame routing. For a drawer, it could be the inner box fastener, connecting element, or technological recess. On a frame-construction facade, the handle zone itself may fall not on a solid plane but on the transition between elements.
The check is performed as an overlay of two maps: the front map of handles and the reverse map of structural elements. The circle of the Cenote mounting seat should not be evaluated in isolation from the other side.
This is especially useful at a minimum thickness of 16 mm. The nominal 4.5 mm obtained after subtracting 11.5 mm applies only to simple geometry without counter-processing. If there is another recess on the reverse side, the mathematical picture changes.
Before a series, it is convenient to make a cross-section of a specific facade through the center of the handle. It shows the total thickness, the Cenote seating depth, and all elements from the reverse side. Such a cross-section answers the question of whether there is a conflict inside the part better than a single frontal diagram.
If the handle position can be slightly changed without violating the design, it is safer to adjust the coordinate at the drawing stage than to try to fix an already milled and painted facade.
Glue and seating: why the mounting description does not become a universal technology
The Cenote card recommends gluing into a prepared recess and names TYTAN Prof. Classic Fix mounting adhesive as the recommended product.
This does not mean that the buyer should independently assign the consumption, adhesive layer thickness, or curing mode based on an article. For that, there is the adhesive instruction and furniture production technology.
From the card for the project, it is enough to extract three facts:
- the handle is recessed;
- a prepared recess is required;
- installation is performed using adhesive.
And the workshop is already checking the facade material, surface preparation, recess cleanliness, and the adhesive working instructions.
The main thing is not to add an "adhesive allowance" to 11.5 mm on your own initiative. The mounting depth should be taken from the approved drawing, not adjusted by guesswork.
What to write in the specification for Cenote HL-029
A ready-made line for procurement and production might look like this:
Cenote HL-029
Product dimensions: 80 × 20 × 66 × 11 mm
Material: beech / oak
Sanding: Prestige
Finish: unpainted
Minimum facade thickness: from 16 mm
Mounting recess: per current drawing; card description — Ø67 × 11.5 mm
Visible protrusion: 9 mm
Quantity: ___ pcs.
Before the series: control fitting on the actual facade material.
In the production version, the X/Y coordinates of each handle, the CNC program number, the facade type, and a sample approval mark are added.
Such a record is much safer than the line “HL-029, Ø66, 20 pcs.” because it does not mix the product size with the installation size.
When not to order Cenote HL-029 yet
Purchase or processing start should be postponed if the facade is thinner than 16 mm or its actual thickness has not yet been measured.
Do not send the series to CNC if the program is built only on the assumption “D=66, E=11 — so it is a cutout.” First, an up-to-date installation drawing is needed.
Cenote is not suitable as an automatic solution if a deep reverse milling, frame construction, or another element that conflicts with the fit passes behind the handle zone.
The model should be reconsidered if the project requires an absolutely zero protrusion above the front surface: after installation, Cenote leaves a visible part of about 9 mm.
If the facades are already finally painted, purchase is possible only after the cabinetmaker has confirmed a safe technology for processing the finished coating. Do not choose a recessed handle at the last minute and shift all the risk onto installation.
Finally, do not order a large batch for the sake of a discount or a deadline before a single control fitting if production has never worked with HL-029 before.
Where to buy Cenote HL-029 and other wooden furniture handles
If the facade design and mounting map are already approved, the final point is the Cenote HL-029 card.
If the model choice is still open, buy wooden furniture handles you can use the general STAVROS section. For a project where hidden mounting is crucial, it is better to immediately look at the specialized selection of recessed models.
The commercial logic for Cenote differs from a regular hardware purchase: first you need to get the handle and mounting data, then allow irreversible facade processing. In this case, the purchase becomes part of the furniture's technological process, not the last decorative decision after painting.
Questions before ordering Cenote HL-029
Why does the card have 66×11 and at the same time Ø67×11.5 mm?
Because 80×20×66×11 mm is the product's dimensional string in the A/C/D/E system, and Ø67×11.5 mm is separately specified in the mounting description as parameters for the recess. They cannot be considered the same pair without checking the drawing.
Is D=66 the cutter diameter?
Automatically no. Dimension D must be read from the drawing. For production sampling, the confirmed mounting dimension is used.
E=11 — is this the depth of the sample?
You should not interpret it by a single letter. In the description, the mounting depth is specified as 11.5 mm.
Which dimension should be sent to the CNC?
The one confirmed by the current Cenote HL-029 mounting drawing and verified by a test fit.
Can Cenote be installed on a 16 mm facade?
The card allows facades with a thickness of 16 mm or more. However, the actual material, back geometry, and processing technology are checked by the furniture manufacturer.
What does the calculation 16 − 11.5 = 4.5 mm mean?
Only the nominal remaining thickness with such geometry. This is not a strength calculation.
Is the handle fully recessed into the facade?
No. The card indicates a visible protrusion of about 9 mm above the surface.
Do I need to buy handles before painting?
For new production, this is rational: a physical handle and a drawing allow checking the fit before final finishing and launching the entire series.
Can I paint the facades first and then make the cutout?
Technologically, this may be possible in a specific production, but the risk of damaging the finished coating is higher. The processing method must be confirmed by the cabinetmaker before starting work.
Is one test fit enough for twenty facades?
If all facades have the same material, thickness, and installation zone construction, one approved sample can serve as a reference. For different types of facades, separate checks are needed.
Is glue included with the handle itself?
The card recommends mounting glue as an accessory. The completeness of a specific order and mounting materials should be checked separately.
How is HL-029 different from HL-029M?
HL-029 is supplied without a ready-made coating and is suitable for project finishing. HL-029M is a separate version with a factory coating.
How to choose between beech and oak?
According to the finishing project and the general furniture specification. If handles are painted together with the fronts, the material still needs to be fixed before ordering the batch.
Will Cenote fit a cabinet in a narrow niche?
You need to check the door trajectory and the 9 mm protrusion. The fact of recessed installation itself does not guarantee the absence of a conflict with the wall or an adjacent front.
What to check on the day of CNC startup?
The current drawing, the diameter and depth of the recess, the actual thickness of the front, X/Y coordinates, the program version, and the result of the test fitting.